Drill Bits Unlimited
0.0625" (1/16", 1.60mm) x .300" LOC 2-Flute Down-Cut Square End Carbide End Mill, 1/8" Shank | M2-140
0.0625" (1/16", 1.60mm) x .300" LOC 2-Flute Down-Cut Square End Carbide End Mill, 1/8" Shank | M2-140
Buy more and Save!
| Minimum Qty | Discount |
|---|---|
| 10 + | 5% off |
| 25 + | 7% off |
| 50 + | 9% off |
| 100 + | 10% off |
Couldn't load pickup availability
1/16" (.0625", Approx. 1.60mm) 2-Flute Down-Cut Square End Carbide End Mill – M2-140
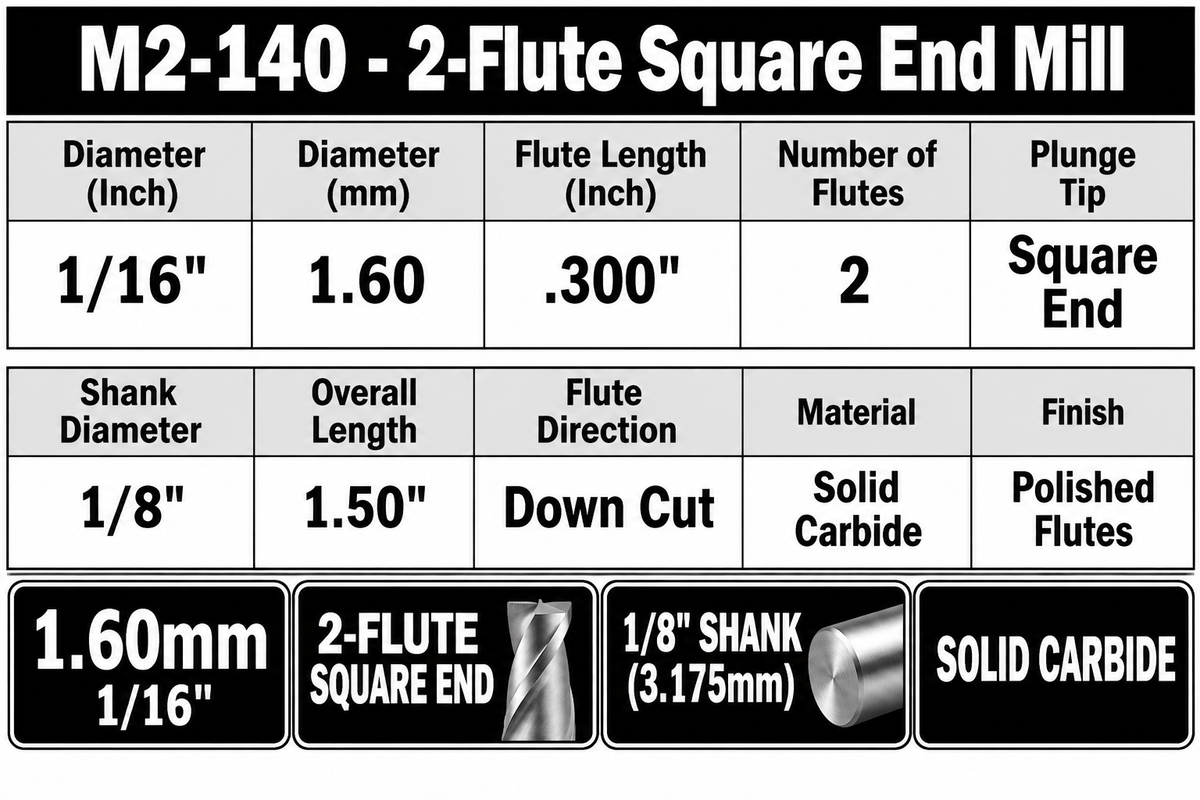
This 1/16" (.0625") solid carbide down-cut end mill features a .300" length of cut, 2-flute square end geometry, 1.50" overall length, polished flutes, and a standard 1/8" shank. Its down-cut geometry is useful for precision CNC milling, profiling, and routing where clean top-surface edges and detailed cutting are important.
Size note: The nominal cutting diameter is 1/16" (.0625"), equivalent to 1.5875mm or approximately 1.60mm. When machining slots or features requiring a precise width, use the nominal fractional or inch diameter rather than the rounded metric reference.
Unlike conventional up-cut end mills, the down-cut spiral geometry directs chips downward toward the workpiece. This can help reduce top-edge lifting, chipping, or fraying in wood, MDF, laminated materials, and certain plastics or composites.
The .300" flute length provides additional cutting reach for narrow profiles, contours, and detailed routing operations. Because down-cut tools direct chips downward, suitable chip removal is particularly important when machining enclosed slots and pockets.
Solid tungsten carbide construction provides rigidity and wear resistance for precision machining. The 2-flute square end geometry is suitable for slots, profiles, contours, pockets, and flat-bottom features when appropriate machining conditions are maintained.
Common Applications
- Precision CNC milling and fine-detail routing
- Clean top-edge cuts in wood, MDF, and suitable sheet materials
- Narrow slotting, profiling, and contouring
- Small pockets and flat-bottom features
- Plastic and acrylic machining
- Laminated sheet and panel materials
- Fine engraving and detailed CNC cutting
- Selected fiberglass and composites with suitable machining parameters
- Selected non-ferrous materials when chip evacuation and cutting conditions are appropriate
Features & Benefits
- 1/16" (.0625") cutting diameter: Suitable for narrow slots, small features, and detailed CNC machining.
- Down-cut spiral geometry: Helps reduce top-edge lifting and fraying in suitable materials.
- .300" flute length: Provides additional cutting reach for narrow profiles and detailed routing.
- 2-flute design: Provides two cutting edges with space for chip evacuation.
- Square end: Suitable for slots, profiles, pockets, contours, and flat-bottom cuts.
- Polished flutes: Provide smooth cutting surfaces.
- Solid tungsten carbide: Provides rigidity and wear resistance.
- 1/8" shank: Compatible with suitable precision CNC collets and toolholders.
Specifications
| SKU | M2-140 |
|---|---|
| Former SKU | M192 |
| Tool Type | Solid Carbide Down-Cut End Mill |
| Condition | New |
| Cutting Diameter | 1/16" / .0625" (1.60mm) |
| Length of Cut / Flute Length | .300" |
| Flutes | 2 |
| End Style | Square End |
| Flute Direction | Down Cut |
| Cut / Helix | Right Cut / Left Helix |
| Overall Length | 1.50" |
| Shank Diameter | 1/8" (3.175mm) |
| Material | Solid Tungsten Carbide |
| Finish | Polished Flutes |
Down-Cut vs. Up-Cut End Mills
Down-cut end mills direct chips downward toward the workpiece, which can help improve top-edge quality in materials prone to lifting, chipping, or fraying.
Up-cut end mills direct chips upward and are often preferable where efficient chip evacuation is the primary concern, particularly in deeper slots and pockets.
Choose flute direction according to the material, desired surface finish, cutting depth, and chip evacuation requirements.
Important Machining Considerations
At just 1/16" cutting diameter with a .300" flute length, this carbide end mill requires careful machining. Use rigid workholding, precision collets, minimal spindle runout, appropriate spindle speeds, controlled cutting depths, and carefully selected feed rates.
Down-cut caution: Because chips are directed downward, avoid allowing chips to accumulate in narrow slots or enclosed pockets. Use suitable chip clearing, conservative passes, and appropriate machining parameters. Excessive chip packing, cutting forces, or tool deflection can lead to poor performance or premature tool breakage.
Explore additional diameters and flute lengths in our Down-Cut Carbide End Mills Collection →
Returns
Returns
Returns are accepted within 30 days of delivery for unused items in resalable condition. Original shipping charges are non-refundable unless the return is due to our error. Late, bulk, used, clearance, or special-order returns may be limited or subject to approval. See our Refund Policy for full details.
Share